Friction drilling enables fast, precise, and durable thread creation in thin materials, directly on your CNC machine. By forming, not cutting, the material, Flowdrill creates a strong, integral bush that provides several times more thread length than the base material thickness.
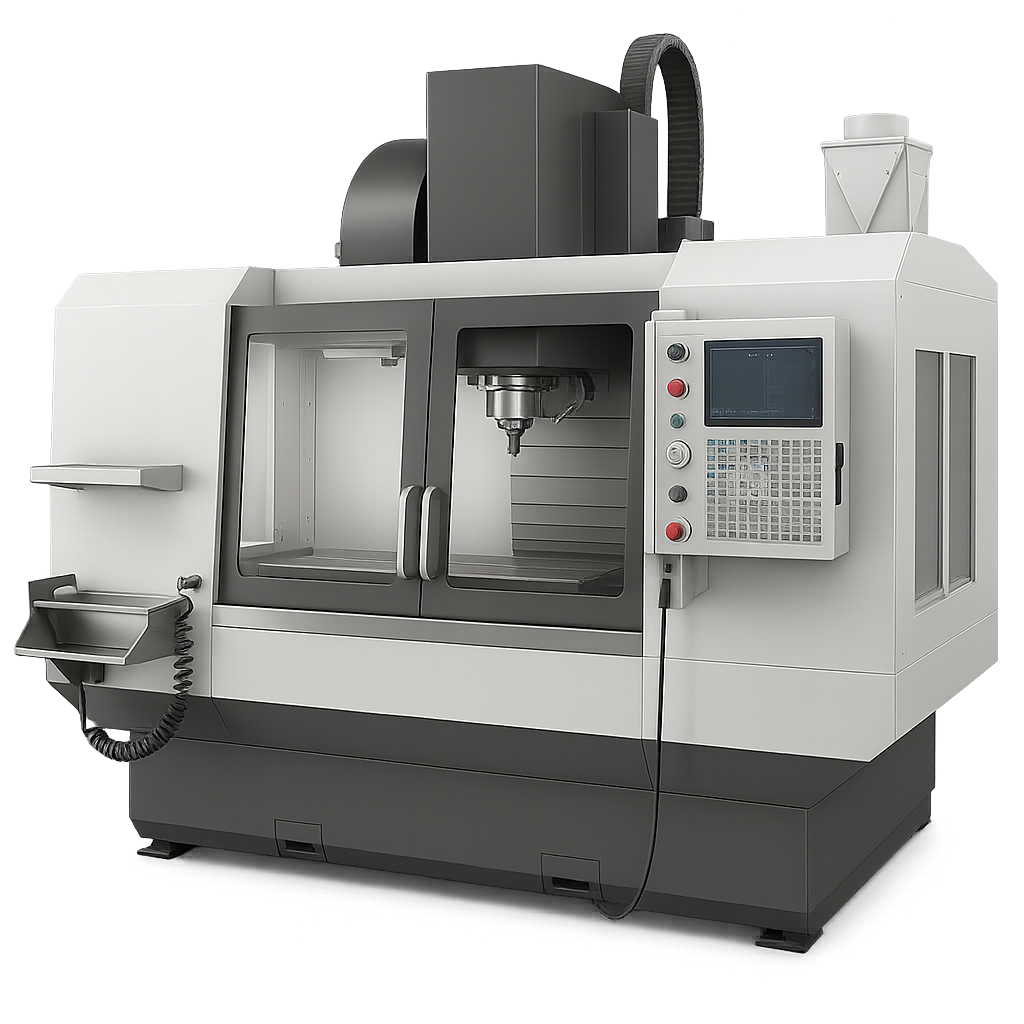
On vertical machining centers (VMC’s) and other CNC setups, friction drilling offers a clean, efficient process for structural and high-load applications.
Key advantages:
Each combination of material and thread size requires a specific CNC program to ensure smooth forming and consistent hole quality.
Provide us with:
We will supply a custom program with the correct spindle speed, feed stages, and cycle time, so you can start right the first time.
For friction drilling and tapping an M8 thread in mild steel (2 mm wall thickness), a Flowdrill tool running at 2180 RPM with programmed feed stages completes the cycle in 2.9 seconds.
| Flowdrill | 7.3 | mm | Short Flat |
| L1 | 13.4 | mm | Working length |
| L4 | 9.4 | mm | |
| Material type | Mild steel | ||
| Wall thickness | Wall thickness 2 mm | ||
| CNC data | |||
| Z | 1.9 | Feed (mm/min) | 100 |
| Z | 3.5 | Feed (mm/min) | 220 |
| Z | 8.0 | Feed (mm/min) | 330 |
| Z | 11.3 | Feed (mm/min) | 530 |
| Z | 13.0 | Feed (mm/min) | 630 |
| Z | 13.4 | Feed (mm/min) | 1000 |
| RPM | 2180 | Cycle time (sec) | 2.9 |
Efficient heat transfer is essential for tool life and spindle safety.
We recommend holders with integrated heat sinks (cooling rings).
Available types:
Our specialists can help select the most cost-effective and stable option for your machine.
Proper lubrication prevents wear and ensures clean threads.
Recommendations:
Application methods:
We can advise on the best setup based on your production speed and automation level.
We’ll help you optimize your CNC process for speed, strength, and repeatability.
To receive a tailored program and setup recommendation, contact our team: